Why Choose Us
- Low VOC & Eco-Friendly: Safe for enclosed spaces and reduces harmful emissions.
- Excellent Chemical Resistance: Protects against oils, cleaning agents, acids, and alkalis.
- Hygienic & Seamless: Ideal for food, pharmaceutical, and clean-room environments.
- UV Stable & Non-Yellowing: Maintains appearance over time.
- Thermal & Impact Resistant: Absorbs shock and withstands temperature changes.
- Slip-Resistant Options: Anti-skid textures available for wet or greasy areas.
- Easy Maintenance: Smooth surface supports quick and effective cleaning.
Types
- Self-Leveling Water Based PU Flooring
- Trowel-Applied Water Based PU Coating
- Food-Grade Water Based PU Flooring
- Pharmaceutical Grade Water Based PU
- Anti-Slip Water Based PU Flooring
- Chemical-Resistant Water Based PU
- High-Build Water Based PU Systems
- Decorative Water Based PU Flooring
- ESD Water Based PU Flooring
- Thermal Shock Resistant Water Based PU
Applications
- Food & Beverage Processing Units
- Dairy & Milk Plants
- Pharmaceutical Clean Rooms
- Commercial Kitchens & Hotels
- Cold Storage & Refrigerated Areas
- Hospitals, Laboratories & Clinics
- Industrial Production Units
- Packaging & Bottling Facilities
- Educational Cafeterias & Kitchens
- Beverage Manufacturing Plants
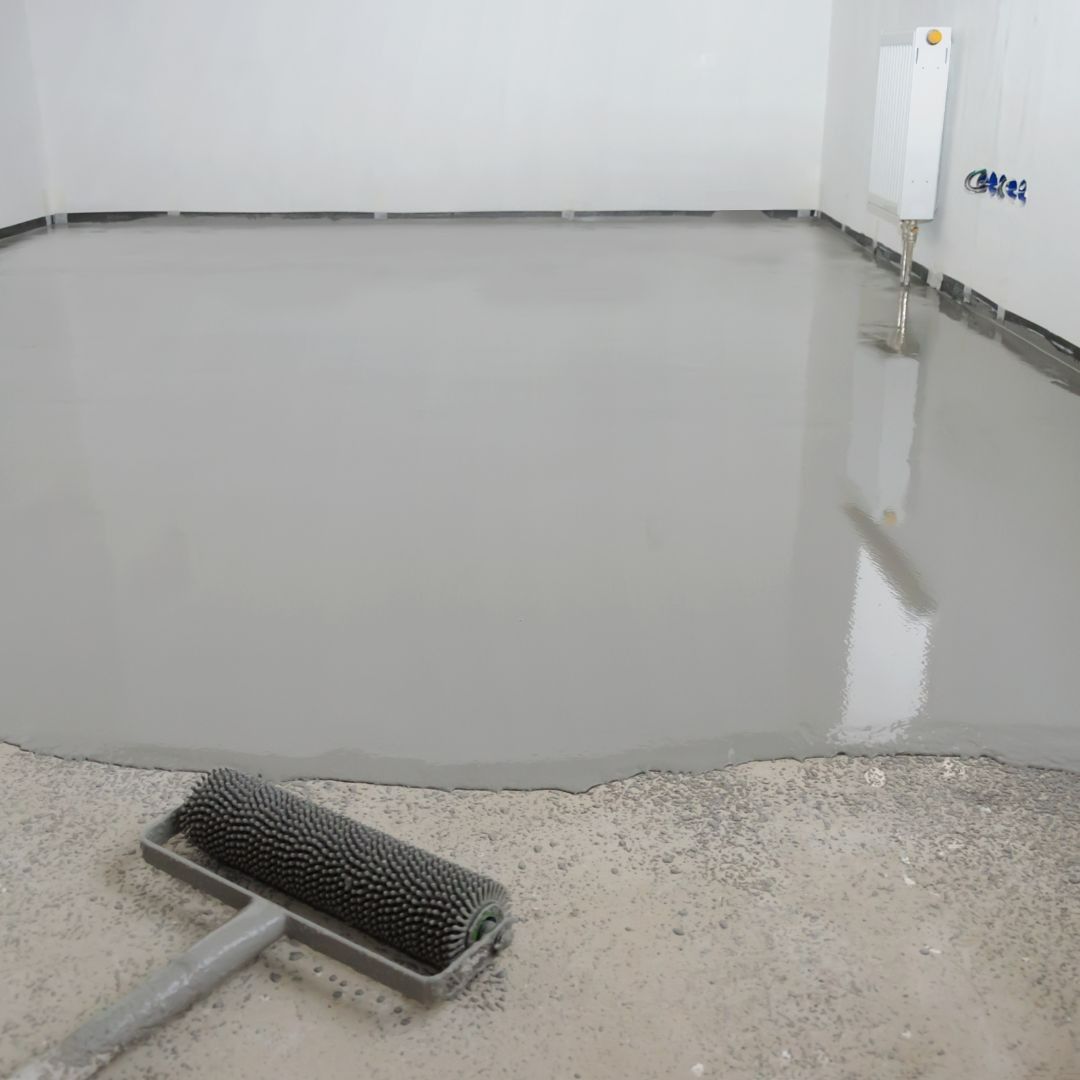
Our professional Water Based PU Flooring installation process includes comprehensive surface preparation, crack treatment, primer application, water-based polyurethane coating, and optional topcoat for enhanced durability. The process involves specialized techniques ensuring optimal adhesion, proper thickness, and seamless finishing. We use advanced application methods creating smooth, joint-free surfaces meeting specific requirements of hygienic and industrial environments.
We follow a systematic approach including thorough surface assessment, proper material selection, precise application, and quality assurance checks. Each installation is customized meeting specific functional requirements, with options for anti-slip textures, custom colors, and high-build coatings based on project needs.
- Surface profiling and thorough cleaning
- Crack treatment and surface defect repair
- Application of epoxy/PU primer for optimal adhesion
- Installation of water-based polyurethane coating
- Optional anti-slip texture application
- Application of protective topcoat for enhanced durability
- Quality inspection and curing period observation
Benefits
- Low VOC & Eco-Friendly: Safe for enclosed spaces and reduces harmful emissions.
- Excellent Chemical Resistance: Protects against oils, cleaning agents, acids, and alkalis.
- Hygienic & Seamless: Ideal for food, pharmaceutical, and clean-room environments.
- UV Stable & Non-Yellowing: Maintains appearance over time.
- Thermal & Impact Resistant: Absorbs shock and withstands temperature changes.
- Slip-Resistant Options: Anti-skid textures available for wet or greasy areas.
- Easy Maintenance: Smooth surface supports quick and effective cleaning.
- Odor-Free Application: Minimal odor during installation, suitable for occupied facilities.
- HACCP Compliance: Meets stringent hygiene standards for food and pharmaceutical industries.
- Long Service Life: Durable construction provides years of reliable performance.
- Improved Indoor Air Quality: Low-VOC formulation enhances workplace safety.
- Versatile Application: Suitable for both new installations and renovation projects.